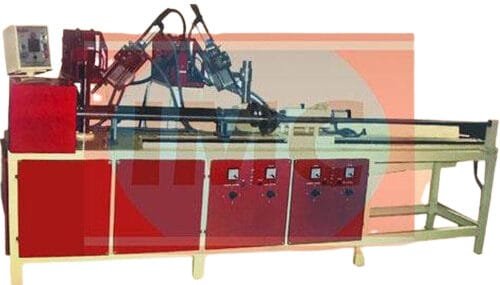
 Heavy Industrial SPM
Model: NCT-SPM-1
Comprehensive Machine Overview
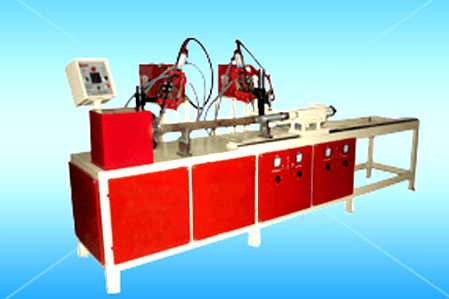
The Horizontal Standard Ledger Welding System is built for automated circumferential welding of cast steel end connectors onto structural scaffold ledger tubes. By rotating the clamped workpiece horizontally between synchronized rotary chucks, the system eliminates the manual repositioning and variable weld penetration common to manual stick or hand MIG welding in high-output scaffolding plants.
The machine uses dual adjustable welding torch mounts linked to a variable-speed rotary drive, enabling simultaneous or sequential fillet welding at both ends of the ledger pipe. A rigid IS 2062 fabricated bed maintains bed alignment across workpiece lengths from 150 mm up to 2400 mm, ensuring concentricity and uniform bead profile conforming to BS EN 12810 and EN 74 structural standards.
Key Features
- Dual-Head MIG Welding: Synchronized torch heads weld both end connectors in a single clamping cycle, cutting cycle time by more than 50%.
- Variable Rotary Speed Control: Inverter-driven headstock spindle allows fine adjustment from 2 to 10 RPM to suit pipe wall thickness.
- Quick-Length Adjust Carriage: Precision linear rack and manual locking handle enable rapid changeovers between 0.5m, 1.0m, 1.5m, and 2.0m ledger lengths.
- Pneumatic Clamping Fixtures: Self-centering pneumatic collets grip 48.3 mm OD tube securely without marring pipe surfaces.
- Standardized Torch Integration: Compatible with all standard industrial MIG power sources including Lincoln, Panasonic, and Kemppi wire feeders.
- Spatter-Shielded Enclosure: Heavy sheet metal sliding shields protect linear ways and operator station from weld spatter.
Applications
- Cuplock system horizontal ledger pipe fabrication
- Ringlock scaffolding ledger and transom welding
- Kwikstage transom and ledger manufacturing
- Tubular structural framing and cross-brace fabrication
Built and assembled at the National Cutting Tools manufacturing facility in Focal Point, Ludhiana. Every machine undergoes a full mechanical run-off and test weld on customer-supplied pipe samples prior to export packing or direct dispatch across India.
High-Yield Production Capabilities & Advantages
Simultaneous Dual-End Seam Welding
Two synchronized welding torches operate at both ends of the ledger pipe simultaneously, eliminating manual flipping and cutting handling time by over 60%.
18–24s Rapid Cycle Time per Ledger
Produces 120 to 160 finished ledgers per hour at 85% operator efficiency, replacing 4 to 5 manual welding booths while using 80% less shop floor space.
4.0–5.5 mm Controlled Penetration
Continuous motorized rotation guarantees uniform fillet throat thickness with zero stop-start cold laps, passing rigorous pull-out and shear load tests.
Zero Spatter on Forged Blade Locking Pockets
Precision wire feed control and tailored shielding gas shrouds protect blade locking pockets from spatter, eliminating manual chiseling before galvanizing.
Pneumatic Rapid Clamping & Ejection Cradle
Heavy pneumatic cylinders secure both ledger heads in 1.5 seconds. A post-weld pneumatic lift cradle unloads finished ledgers directly onto gravity transfer tables.
Engineering Data Matrix
| Technical Parameter | Operational Specification / Value |
|---|---|
| Electric Supply | Single Phase 220 Volt HZ 50/60 |
| Speed | 2 To 10 rpm |
| Motor Drive | AC Inverter Type |
| Motor-Type | AC 220-Volts-3-Phase |
| Torch Clamping | PNEUMATIC |
| Length Adjustment | 150 To 2400 Mm |
| Dimension | L X W X H 11.3×2.5×5.3 (Foot) |
Machine Architecture & Mechanical Construction
Stress-Relieved Machine Bed (IS 2062)
Heavy-duty chassis fabricated from IS 2062 structural steel channels and 25 mm thick ground steel plates. Thermally stress-relieved prior to multi-axis plano-milling.
Hardened Spindle & Precision Headstock
Induction-hardened EN8/EN9 alloy steel main spindle on heavy tapered roller bearings, driven by a 1.5 HP motor and Delta VFD for backlash-free rotational starts and stops.
Tailstock & Quick-Change Ledger Tooling
Adjustable tailstock on induction-hardened guide shafts. Drop-in, case-hardened alloy tool-steel fixtures accommodate Cuplock blades, Ringlock heads, or Kwikstage wedges in under 10 minutes.
IP54 Dust-Proof Industrial Electrical Cabinet
Isolated, forced-air cooled IP54 electrical enclosure housing Delta/Mitsubishi PLC, touch HMI screen, and universal dry-contact trigger interfaces for Lincoln, Panasonic, and Kemppi.
Industrial Plant Integration & Fabrication Flow
Balanced production beat eliminating fabrication queue bottlenecks.
Precision Pipe Cutting
Cold saw cutting of raw IS 2062 / EN 10219 pipe into exact ledger lengths (500 mm – 3000 mm) with 90° square cut faces.
Pipe End Chamfering
Automatic pipe end-facing removes inner and outer burrs, ensuring 100% flush root fit-up against forged blade weld shoulders.
Dual-Torch MIG Welder
NCT dual-torch SPM strikes simultaneous arcs, completing twin 360°+15° circumferential welds within 18–24 seconds.
QA & Galvanizing
Batch tensile pull testing followed by immediate transfer to acid pickling and molten zinc hot-dip galvanizing baths.
Horizontal Standard Ledger Welding System Works QA & Export Packaging Protocol
✓ Circumferential Arc & Pneumatic Alignment Trials
- • Rotary Spindle Concentricity: Spindle chuck and pneumatic tailstock axial alignment verified within 0.08 mm to ensure uniform rotation without tube run-out.
- • Continuous Arc Cycle Testing: Minimum 25 continuous 360-degree weld runs executed on sample pipes to verify torch angle, arc stability, and bead penetration.
- • Macro-Etch Penetration Check: Cut-section metallurgical inspection of weld beads to confirm root penetration meeting BS 1139 and EN 12810 standards.
- • Run-Off Video Recording: Trial welding cycle on your specified tube diameter recorded in HD and shared for formal technical sign-off prior to dispatch.
Seaworthy Automated Station Packaging (ISPM-15)
- • Torch Carriage Bracing: Pneumatic slides, welding torch brackets, and rotary spindles locked with heavy-duty mechanical transport braces.
- • VCI Moisture Protection: Copper heat sinks, clamping jaws, and bare electrical contacts treated with volatile corrosion inhibitor (VCI) film.
- • Solid Timber Crating: Fumigated ISPM-15 certified solid pine wood crate with waterproof polyethylene outer envelope.
- • Container Lashing Points: Heavy structural skid base with internal corner tie-down brackets for ocean container transport.
International Shipping Destinations & India Supply Network
National Cutting Tools manufactures and configures the Horizontal Standard Ledger Welding System for seamless integration into international fabrication lines and domestic scaffolding manufacturing plants. All machinery is customized for local electrical grids, certified for regional compliance, and dispatched with seaworthy protective packaging.
Primary International Export Destinations
All Export Hubs →Pan-India Fast Freight Dispatch (Ludhiana Works)
India Directory →Full-truckload (FTL) and part-load freight dispatch directly from our central manufacturing works at Focal Point, Ludhiana. Factory engineers provide on-site leveling, tool alignment, and operator training across all major industrial manufacturing clusters:
Frequently Asked Questions • Horizontal Standard Ledger Welding System
Direct Factory Machinery Proposal
Connect with our engineering specialists in Ludhiana. Receive comprehensive technical specifications, power requirements, tooling options, and estimated FOB/CIF maritime rates.
Request Formal Quotation
Please provide production requirements for exact tooling design.
Scaffolding Manufacturing Machinery: The Complete Plant Setup Guide
Technical breakdown covering machine sizing, tooling die setups, cycle speeds, and operational maintenance for Scaffolding Machinery.