 Heavy Industrial SPM
Model: NCT-BJW-400
Comprehensive Machine Overview
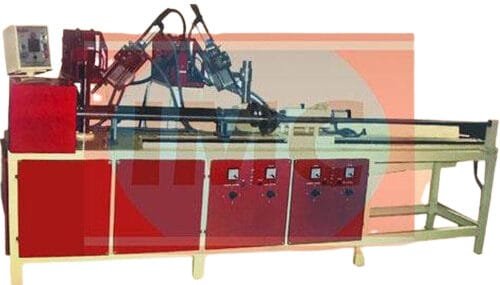
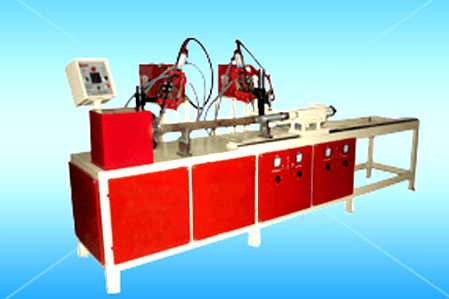
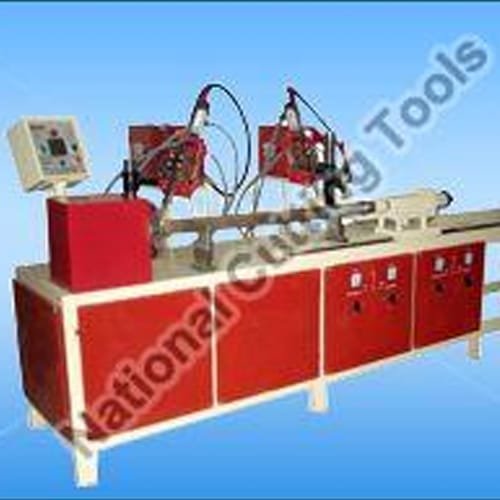
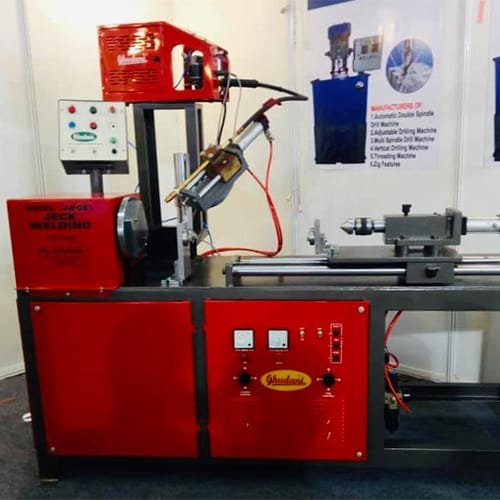
The Base And U-Head Jack Welding Machine is a dedicated industrial system engineered by National Cutting Tools for <p>The Base and U-Head Jack Welding Machine is an automated welding workstation built specifically for manufacturing scaffolding leveling jacks. Leveling jacks support the entire dead and live load of falsework towers; a defective or incomplete weld between the solid or hollow screw rod and the base plate can result in sudden structural collapse. This machine automates the full 360-degree fillet weld to deliver deep, crack-free penetration.</p>.
<p>The unit features a vertical or horizontal chuck assembly with pneumatic top-clamping to hold the threaded stem dead perpendicular to the base plate or U-head channel. An automated rotary drive turns the assembly under a fixed MIG welding torch, laying down a consistent 6 mm to 8 mm fillet bead around the base joint in less than 20 seconds.</p>
<h3>Key Features</h3>
<ul>
<li><strong>Perpendicular Alignment Clamping:</strong> Heavy pneumatic cylinder clamps the base plate flat against the screw stem to guarantee true 90-degree squareness.</li>
<li><strong>Automated Circular Torch Trajectory:</strong> Synchronized rotation ensures consistent fillet throat thickness without spatter in the screw threads.</li>
<li><strong>Thread Protection Tooling:</strong> Copper collets and protective shielding prevent stray arc strikes and weld spatter on precision rolled threads.</li>
<li><strong>Dual-Purpose Fixture Design:</strong> Rapid-change tooling holds both 150x150 mm flat base plates and formed 100x150 mm U-head top channels.</li>
<li><strong>Foot Pedal Cycle Initiation:</strong> Allows the operator to position components with both hands before initiating the automated pneumatic clamp and weld sequence.</li>
</ul>
<h3>Applications</h3>
<ul>
<li>Scaffolding adjustable base jack plate welding</li>
<li>Formwork U-head jack and universal jack fabrication</li>
<li>Shoring tower leveling spindle assembly</li>
<li>Heavy-duty screw jack foot attachment</li>
</ul>
<p>Built at the NCT manufacturing facility in Ludhiana, Punjab. Every unit is tested with full pneumatic clamping pressure and test welds on production plates before release for dispatch across India and overseas export.</p>
High-Yield Production Capabilities & Advantages
Simultaneous Perimeter Fillet Welding
Rotary MIG torches lay continuous circumferential fillets around 32mm to 48mm threaded screw rods in 16–22 seconds.
100% Perpendicularity Guarantee
Heavy pneumatic clamping ram presses base plates flat against the rotary fixture, ensuring strict 90° axial alignment under heavy loads.
Dual Base Plate & U-Head Tooling
Interchangeable magnetic and mechanical jigs handle flat base plates (150×150 mm) or heavy channel U-heads with rapid changeover.
Deep Root Weld Penetration
Multi-torch MIG configuration provides 5.0–6.0 mm throat penetration, withstanding 200+ kN ultimate compressive and tensile loads.
High-Speed Automated Output
Produces 140 to 180 completed base jacks per hour, dramatically surpassing manual welding tables with zero defect rejects.
Engineering Data Matrix
| Technical Parameter | Operational Specification / Value |
|---|---|
| Drive | A.C. Motor |
| R.P.M. | 2 to 10 |
| Operation | Pneumatic |
| Air Pressure Required | 4 to 5 Bar |
| Length Adjustment | 150 to 950 mm |
| Power Supply | 1 Phase (220V ±5%) / 3 Phase (415V ±5%) |
| Power Consumption | 1 KVA to Max. 9 KVA |
| Frequency | 50/60 Hz |
| Operating Voltage | 24 Volts |
| Control System | Touch Screen / Digital |
| Production Capacity | Approx. 500–550 Pieces |
| Dimensions (L × W × H) | 5.4 × 2.5 × 4.7 Feet (Approx.) |
| Country of Origin | India |
Machine Architecture & Mechanical Construction
Rigid Structural Steel Column & Base
Constructed from heavy IS 2062 plate, normalized to absorb shock loads and prevent thermal deflection during continuous welding.
Heavy Pneumatic Top-Locking Cylinder
High-thrust pneumatic cylinder delivers up to 1200 kg clamping force, holding the base plate dead flat during rotary welding.
Hardened Hollow Spindle & Rotary Earth
EN9 alloy spindle with copper rotary earth brush system, preventing high-amperage electrical arcing inside mechanical bearings.
Automated PLC Control Console
Microprocessor/PLC sequencing with programmable rotation speed, pre-weld gas purge, and crater-fill overlap.
Industrial Plant Integration & Fabrication Flow
Balanced production beat eliminating fabrication queue bottlenecks.
Threaded Rod & Plate Prep
Jack screw rod cut to length; base plates punched and countersunk.
Pneumatic Ram Lock
Plate and threaded rod loaded into self-aligning rotary jig and locked.
Automatic MIG Weld
Twin MIG torches deposit 360° full fillet weld in 16–22 seconds.
Axial Load Test & Galvanizing
Proof compression testing followed by hot-dip zinc galvanizing.
Base And U-Head Jack Welding Machine Works QA & Export Packaging Protocol
✓ Circumferential Arc & Pneumatic Alignment Trials
- • Rotary Spindle Concentricity: Spindle chuck and pneumatic tailstock axial alignment verified within 0.08 mm to ensure uniform rotation without tube run-out.
- • Continuous Arc Cycle Testing: Minimum 25 continuous 360-degree weld runs executed on sample pipes to verify torch angle, arc stability, and bead penetration.
- • Macro-Etch Penetration Check: Cut-section metallurgical inspection of weld beads to confirm root penetration meeting BS 1139 and EN 12810 standards.
- • Run-Off Video Recording: Trial welding cycle on your specified tube diameter recorded in HD and shared for formal technical sign-off prior to dispatch.
Seaworthy Automated Station Packaging (ISPM-15)
- • Torch Carriage Bracing: Pneumatic slides, welding torch brackets, and rotary spindles locked with heavy-duty mechanical transport braces.
- • VCI Moisture Protection: Copper heat sinks, clamping jaws, and bare electrical contacts treated with volatile corrosion inhibitor (VCI) film.
- • Solid Timber Crating: Fumigated ISPM-15 certified solid pine wood crate with waterproof polyethylene outer envelope.
- • Container Lashing Points: Heavy structural skid base with internal corner tie-down brackets for ocean container transport.
International Shipping Destinations & India Supply Network
National Cutting Tools manufactures and configures the Base And U-Head Jack Welding Machine for seamless integration into international fabrication lines and domestic scaffolding manufacturing plants. All machinery is customized for local electrical grids, certified for regional compliance, and dispatched with seaworthy protective packaging.
Primary International Export Destinations
All Export Hubs →Pan-India Fast Freight Dispatch (Ludhiana Works)
India Directory →Full-truckload (FTL) and part-load freight dispatch directly from our central manufacturing works at Focal Point, Ludhiana. Factory engineers provide on-site leveling, tool alignment, and operator training across all major industrial manufacturing clusters:
Frequently Asked Questions • Base And U-Head Jack Welding Machine
Direct Factory Machinery Proposal
Connect with our engineering specialists in Ludhiana. Receive comprehensive technical specifications, power requirements, tooling options, and estimated FOB/CIF maritime rates.
Request Formal Quotation
Please provide production requirements for exact tooling design.
Scaffolding Manufacturing Machinery: The Complete Plant Setup Guide
Technical breakdown covering machine sizing, tooling die setups, cycle speeds, and operational maintenance for Scaffolding Machinery.