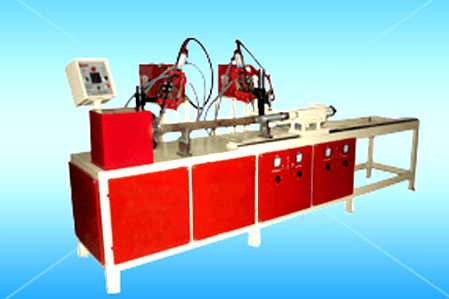
 Heavy Industrial SPM
Model: NCT-LWM-500
Comprehensive Machine Overview
Manual welding of scaffolding horizontal ledgers is the single biggest operational bottleneck in commercial formwork fabrication shops. Fabricating standard Cuplock, Ringlock, or Kwikstage ledgers requires joining two forged steel ledger blades (cast or drop-forged carbon steel) to both ends of a 48.3 mm nominal OD pipe. Manual stick or manual MIG welding causes inconsistent root penetration, weld spatter inside forged ears, human fatigue, weld porosity, and angular run-out. Crucially, a certified welder manually turning pipes can rarely complete more than 18–25 ledgers per hour, with high reject rates during third-party client inspections.
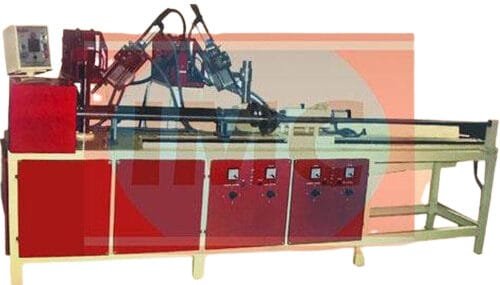
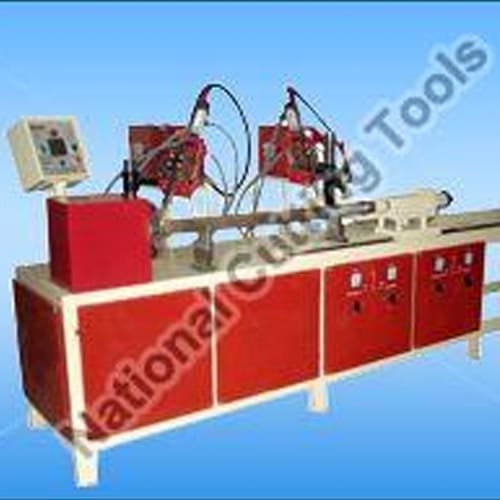
The National Cutting Tools Automatic Double Torch Ledger Welding Machine is a dedicated special-purpose machine (SPM) engineered to mechanize and synchronize this operation. Operating on a rigid, stress-relieved structural steel bed, the machine uses two coordinated pneumatic clamping heads, a variable-speed rotary spindle drive, and twin MIG welding torches that strike arcs simultaneously at both pipe ends.
By automating the torch angle, pre-gas flow, torch travel, arc-strike timing, rotary overlap (360° plus 15° crater-fill overlap), and torch retract cycles, this machine completes both circumferential welds in 18 to 24 seconds (depending on pipe wall thickness). Designed for continuous 2-shift and 3-shift industrial duty cycles, it delivers uniform weld beads that comply with international structural safety standards, including BS 1139-1.1, EN 74-1, and OSHA 1926.451.
High-Yield Production Capabilities & Advantages
Simultaneous Dual-End Seam Welding
Two synchronized welding torches operate at both ends of the ledger pipe simultaneously, eliminating manual flipping and cutting handling time by over 60%.
18–24s Rapid Cycle Time per Ledger
Produces 120 to 160 finished ledgers per hour at 85% operator efficiency, replacing 4 to 5 manual welding booths while using 80% less shop floor space.
4.0–5.5 mm Controlled Penetration
Continuous motorized rotation guarantees uniform fillet throat thickness with zero stop-start cold laps, passing rigorous pull-out and shear load tests.
Zero Spatter on Forged Blade Locking Pockets
Precision wire feed control and tailored shielding gas shrouds protect blade locking pockets from spatter, eliminating manual chiseling before galvanizing.
Pneumatic Rapid Clamping & Ejection Cradle
Heavy pneumatic cylinders secure both ledger heads in 1.5 seconds. A post-weld pneumatic lift cradle unloads finished ledgers directly onto gravity transfer tables.
Engineering Data Matrix
| Technical Parameter | Operational Specification / Value |
|---|---|
| Type | Welding Machine |
| Material | Stainless Steel |
| Welding Type | MIG, Or TIG Welding |
| Speed Range | 1 To 10 Meters Per Minute |
| Phase | Three Phase |
| Surface Finish | Polished |
| Welding Capacity | Up To 12mm Thick |
| Input Power | 8 -10 KW |
| Welding Electrode Size | 1.6mm To 4.0mm |
| Cooling System | Water- Cooled |
| Frequency | 50Hz |
| Operator Interface | Touchscreen Panel |
| Welding Current | 100A To 300A |
| Application | Construction And Industrial |
| Maintenance Required | Low Maintenance |
| Safety Features | Overload Protection, Emergency Stop Button, Safety Guard |
| Country Of Origin | India |
Machine Architecture & Mechanical Construction
Stress-Relieved Machine Bed (IS 2062)
Heavy-duty chassis fabricated from IS 2062 structural steel channels and 25 mm thick ground steel plates. Thermally stress-relieved prior to multi-axis plano-milling.
Hardened Spindle & Precision Headstock
Induction-hardened EN8/EN9 alloy steel main spindle on heavy tapered roller bearings, driven by a 1.5 HP motor and Delta VFD for backlash-free rotational starts and stops.
Tailstock & Quick-Change Ledger Tooling
Adjustable tailstock on induction-hardened guide shafts. Drop-in, case-hardened alloy tool-steel fixtures accommodate Cuplock blades, Ringlock heads, or Kwikstage wedges in under 10 minutes.
IP54 Dust-Proof Industrial Electrical Cabinet
Isolated, forced-air cooled IP54 electrical enclosure housing Delta/Mitsubishi PLC, touch HMI screen, and universal dry-contact trigger interfaces for Lincoln, Panasonic, and Kemppi.
Industrial Plant Integration & Fabrication Flow
Balanced production beat eliminating fabrication queue bottlenecks.
Precision Pipe Cutting
Cold saw cutting of raw IS 2062 / EN 10219 pipe into exact ledger lengths (500 mm – 3000 mm) with 90° square cut faces.
Pipe End Chamfering
Automatic pipe end-facing removes inner and outer burrs, ensuring 100% flush root fit-up against forged blade weld shoulders.
Dual-Torch MIG Welder
NCT dual-torch SPM strikes simultaneous arcs, completing twin 360°+15° circumferential welds within 18–24 seconds.
QA & Galvanizing
Batch tensile pull testing followed by immediate transfer to acid pickling and molten zinc hot-dip galvanizing baths.
Ludhiana Works QA & Export Packaging Protocol
✓ 48-Hour Pre-Dispatch Run-Off Trials
- • Geometric Alignment: Spindle run-out validation on headstock and tailstock within 0.05 mm using dial test indicators (DTI).
- • Live Arc / Forming Trials: Minimum 25 live continuous operational cycles conducted on actual client tube/metal samples.
- • Electrical & PLC Audit: Full 48-hour burn-in testing of PLC relays, touch screen HMI, and motor thermal limits under full rated load.
- • Run-off recording: The machine is run on your material before crating and the run can be recorded and sent to you for sign-off.
Seaworthy International Packaging (ISPM-15)
- • Corrosion protection: Unpainted machined surfaces, spindles and guide rails are treated with a rust inhibitor and wrapped against moisture for the crossing.
- • Moisture Desiccant Packs: Silica gel packs placed inside electrical cabinets to prevent condensation during humid maritime transit.
- • ISPM-15 Heat-Treated Crating: Solid timber skids and fully enclosed wooden boxes stamped with phytosanitary compliance marks.
- • Container Mooring Points: Heavy-duty internal tie-down brackets ensure zero machine movement inside 20ft/40ft ocean containers.
Frequently Asked Technical Questions
Direct Factory Machinery Proposal
Connect with our engineering specialists in Ludhiana. Receive comprehensive technical specifications, power requirements, tooling options, and estimated FOB/CIF maritime rates.
Request Formal Quotation
Please provide production requirements for exact tooling design.