 Heavy Industrial SPM
Model: NCT-RWM-STD
Comprehensive Machine Overview
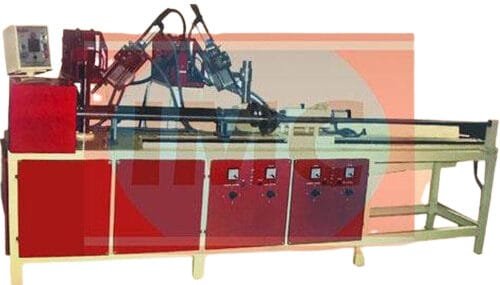
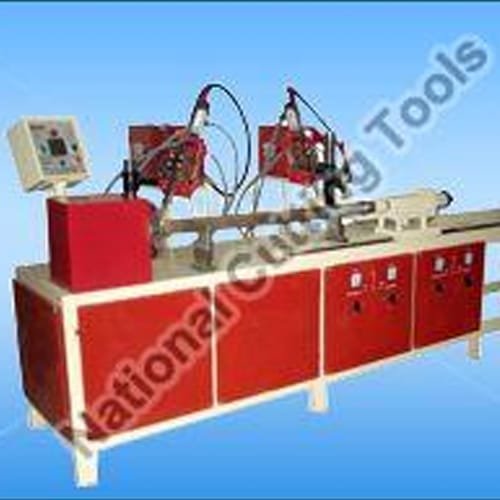
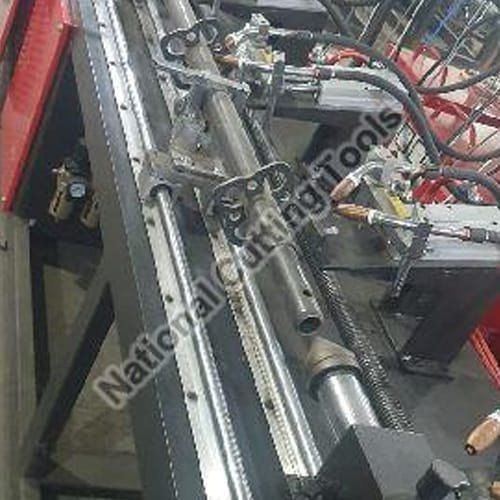
Designed to maintain strict dimensional tolerances under continuous multi-shift production, the Standard Ringlock Welding Machine provides <p>The Standard Ringlock Welding Machine is an automated special-purpose machine engineered for circular MIG welding of 8-hole Ringlock rosettes onto 48. 3 mm nominal OD vertical standards. Attaching multi-rosette clusters manually results in angular misalignment, spatter buildup in rosette wedge pockets, and inconsistent penetration that can cause failure during EN 12810 structural pull-out testing.</p>.
<p>Constructed on a heavy, stress-relieved IS 2062 chassis, the machine features dual synchronized MIG torches, an induction-hardened hollow spindle drive, and a linear rail with pneumatic indexing stops at exact 500 mm center-to-center pitch intervals. The machine completes circumferential welds with programmable 15-degree overlap around each rosette in 25 to 35 seconds per cluster, replacing up to four manual welding stations.</p>
<h3>Key Features</h3>
<ul>
<li><strong>Dual Synchronized MIG Torches:</strong> Welds top and bottom circular fillets simultaneously, balancing heat input to prevent tube distortion.</li>
<li><strong>500 mm Linear Indexing Pitch:</strong> Hardened gauge stops ensure precise standard spacing across pipe lengths of 0.5 m, 1.0 m, 1.5 m, 2.0 m, and 3.0 m.</li>
<li><strong>PLC & Touchscreen HMI Interface:</strong> Stores multiple recipe parameters for wire feed speed, rotation RPM, pre-flow, and crater-fill timing.</li>
<li><strong>Integrated Rosette Positioning Jigs:</strong> Case-hardened locating fixtures position rosettes at exact 90-degree and 45-degree orientations with spatter shielding.</li>
<li><strong>Pneumatic Clamping & Ejection:</strong> Centers the tube on the spindle axis in under two seconds and lifts finished standards onto roll-off skids.</li>
<li><strong>Wide Grid Voltage Compatibility:</strong> Built for 380V/415V 50Hz/60Hz grids with industrial Schneider/Siemens switchgear for GCC and European export markets.</li>
</ul>
<h3>Applications</h3>
<ul>
<li>Ringlock scaffolding vertical standard (upright) fabrication</li>
<li>Modular all-round scaffolding manufacturing</li>
<li>Heavy shoring tower vertical component production</li>
<li>High-volume scaffold export production lines</li>
</ul>
<p>Manufactured and fully assembled at National Cutting Tools in Focal Point, Ludhiana. Pre-dispatch inspection includes sample welding, rosette pitch tolerance checks (within ±0.5 mm), and weld penetration validation.</p>
High-Yield Production Capabilities & Advantages
Multi-Torch Simultaneous Rosette Welding
Dual synchronized MIG torches weld top and bottom circular fillets around each rosette simultaneously, preventing thermal distortion and cutting cycle times by 65%.
25–35s Rapid Cycle Time per Cluster
Achieves continuous production of 80 to 110 completed rosette joints per hour at 85% operator efficiency, replacing up to 4 manual certified welding stations.
4.0–5.5 mm Controlled Fillet Throat
Continuous motorized rotation eliminates start-stop cold laps, producing deep, spatter-free weld beads meeting stringent BS 1139 and EN 12810 structural pull-out criteria.
Precision 500 mm Rosette Indexing Pitch
Hardened linear indexing rail and pneumatic gauge blocks guarantee exact 500 mm center-to-center pitch tolerance (within ±0.5 mm) across standards up to 3000 mm.
Pneumatic Tube Clamping & Auto-Ejection
Heavy-duty pneumatic self-centering chucks lock raw pipe in 1.5 seconds. A post-weld pneumatic lift cradle unloads the hot vertical standard directly onto gravity discharge rollers.
Engineering Data Matrix
| Technical Parameter | Operational Specification / Value |
|---|---|
| Model Designation | NCT-RWM-STD |
| Input Pipe Diameter | 48.3 mm (OD) |
| Pipe Wall Thickness Scope | 2.5 mm to 4.0 mm |
| Standard Rosette Pitch | 500 mm Standard (Adjustable) |
| Length Adjustment Range | 500 mm to 3000 mm |
| Torch Travel / Indexing | Pneumatic / Rotary Mechanical Indexing |
| Operating Cycle Time | 25 to 35 seconds per rosette cluster |
| Welding Power Source Compatibility | 350A / 500A Inverter MIG/MAG (Multi-Torch) |
| Pneumatic Air Consumption | 6 to 8 Bar (Clean Dry Air) |
| Control System | Delta / Mitsubishi PLC with Touch Screen HMI |
| Electrical Power Supply | 380V / 415V, 3-Phase, 50/60 Hz |
| Operating Voltage | 24V DC Safe Control Circuit |
| Production Yield | 80 to 110 rosette joints per hour |
| Dimensions (L × W × H) | 4500 × 900 × 1600 mm Approx. |
| Machine Weight | 2200 Kgs Approx. |
| Chassis Frame Material | Heavy Stress-Relieved IS 2062 Steel |
| Factory Pre-Dispatch Run-Off | 100% Tested on Live Pipe Samples with Video Protocol |
Machine Architecture & Mechanical Construction
Stress-Relieved Chassis Bed (IS 2062)
Constructed from heavy 25 mm thick structural steel plate and heavy box-channels, thermally normalized and plano-milled to preserve sub-millimeter axial alignment across 3.5-meter bed spans.
Induction-Hardened EN8/EN9 Spindle
Large-bore hollow spindle machined from EN8/EN9 alloy steel, rotating on heavy pre-loaded tapered roller bearings driven by a 2.0 HP motor with variable frequency speed regulation.
Precision Rosette Positioning & Spatter Shields
Drop-in case-hardened jigs locate 8-hole Ringlock rosettes at exact 90° and 45° orientations. Integrated copper spatter guards protect rosette wedge slots from stray molten metal.
IP54 Dust-Proof Electrical Enclosure
Forced-air cooled IP54 cabinet housing Delta/Mitsubishi PLC, color touchscreen HMI, Schneider switchgear, and universal multi-pin trigger interfaces for Lincoln, Panasonic, and OTC power sources.
Industrial Plant Integration & Fabrication Flow
Balanced production beat eliminating fabrication queue bottlenecks.
Pipe Cold Sawing
Raw 48.3 mm OD steel tube is cut to finished standard length (1m to 3m) with square, burr-free ends.
Rosette Position Jigs
Pre-stamped 8-hole rosettes are placed into pneumatic locator fixtures along the linear indexing rail.
NCT Ringlock MIG Welder
Dual MIG torches strike simultaneous circular arcs, completing 360°+15° crater fill in 25–35 seconds.
Proof Test & Galvanizing
Rosette weld joints undergo 100 kN torque/pull-out proof testing prior to hot-dip galvanizing baths.
Standard Ringlock Welding Machine Works QA & Export Packaging Protocol
✓ Circumferential Arc & Pneumatic Alignment Trials
- • Rotary Spindle Concentricity: Spindle chuck and pneumatic tailstock axial alignment verified within 0.08 mm to ensure uniform rotation without tube run-out.
- • Continuous Arc Cycle Testing: Minimum 25 continuous 360-degree weld runs executed on sample pipes to verify torch angle, arc stability, and bead penetration.
- • Macro-Etch Penetration Check: Cut-section metallurgical inspection of weld beads to confirm root penetration meeting BS 1139 and EN 12810 standards.
- • Run-Off Video Recording: Trial welding cycle on your specified tube diameter recorded in HD and shared for formal technical sign-off prior to dispatch.
Seaworthy Automated Station Packaging (ISPM-15)
- • Torch Carriage Bracing: Pneumatic slides, welding torch brackets, and rotary spindles locked with heavy-duty mechanical transport braces.
- • VCI Moisture Protection: Copper heat sinks, clamping jaws, and bare electrical contacts treated with volatile corrosion inhibitor (VCI) film.
- • Solid Timber Crating: Fumigated ISPM-15 certified solid pine wood crate with waterproof polyethylene outer envelope.
- • Container Lashing Points: Heavy structural skid base with internal corner tie-down brackets for ocean container transport.
International Shipping Destinations & India Supply Network
National Cutting Tools manufactures and configures the Standard Ringlock Welding Machine for seamless integration into international fabrication lines and domestic scaffolding manufacturing plants. All machinery is customized for local electrical grids, certified for regional compliance, and dispatched with seaworthy protective packaging.
Primary International Export Destinations
All Export Hubs →Pan-India Fast Freight Dispatch (Ludhiana Works)
India Directory →Full-truckload (FTL) and part-load freight dispatch directly from our central manufacturing works at Focal Point, Ludhiana. Factory engineers provide on-site leveling, tool alignment, and operator training across all major industrial manufacturing clusters:
Frequently Asked Questions • Standard Ringlock Welding Machine
Direct Factory Machinery Proposal
Connect with our engineering specialists in Ludhiana. Receive comprehensive technical specifications, power requirements, tooling options, and estimated FOB/CIF maritime rates.
Request Formal Quotation
Please provide production requirements for exact tooling design.
Scaffolding Manufacturing Machinery: The Complete Plant Setup Guide
Technical breakdown covering machine sizing, tooling die setups, cycle speeds, and operational maintenance for Scaffolding Machinery.