A detailed engineering guide comparing C-frame, 4-pillar, and H-frame hydraulic presses. Analyzes deep drawing dynamics, hydraulic cushion tonnage, ram speed control, manifold block valving, and bed deflection limits.
Industrial Hydraulic Press Engineering for Stamping and Forming
From deep-drawn automotive filter shells, stainless steel kitchen sinks, and LPG cylinder ends to heavy structural punching and scaffolding component pressing, hydraulic presses provide controllable, full-tonnage pressure throughout the entire ram stroke. Unlike mechanical crank presses whose force peaks strictly at bottom dead center, hydraulic presses deliver constant programmed force, adjustable dwell times, and precise speed transitions essential for complex metal flow operations.
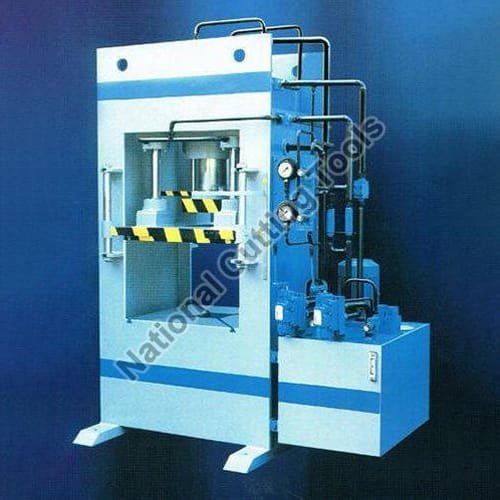
At National Cutting Tools in Ludhiana, our press manufacturing division builds C-frame hydraulic presses, 4-pillar double action deep drawing presses, and heavy H-frame fabrication presses. This guide provides technical specifications for selecting the right press structure.
1. Press Architectural Frame Structures
- C-Frame (Gap Frame) Hydraulic Presses: Open on three sides, providing open accessibility for manual part loading, automated robotic arm access, and long component insertion. Ideal for punch pressing, straightening, bearing pressing, and light drawing up to 250 tons. Requires heavy stress-relieved side plates to prevent "frame gaping" (angular frame deflection under peak tonnage).
- 4-Pillar (Four Column) Presses: Four precision-ground, hard chrome-plated alloy steel columns guide the moving platen. Delivers uniform load distribution, accessible die access from all 4 directions, and accommodates eccentric loading better than open-back designs. The industry standard for deep drawing, rubber vulcanizing, and composite moulding up to 1000 tons.
- H-Frame / Straight-Side Presses: Massive closed-box frame construction fabricated from ultrasonic-tested IS 2062 plate. Ultra-rigid 8-point bronze gib slides guide the slide platen, eliminating lateral deflection during progressive die stamping and heavy offset blanking.
2. Deep Drawing Mechanics: Double Action vs Die Cushion
Deep drawing sheet metal requires two distinct forces working in coordination:
- The Blank Holder (Binder) Force: Prevents wrinkling and flange puckering as the sheet metal flows into the die cavity.
- The Main Drawing Punch Force: Pushes the metal into the die to form the cup, cylinder, or dome shape.
In NCT double-action presses, the blank holder slide advances first, grips the sheet perimeter under calibrated hydraulic pressure, and holds it firmly while the central drawing punch descends. Alternatively, single-action presses can be equipped with a bottom hydraulic die cushion located inside the bed casting, functioning as a blank holder or part ejector with variable pneumatic/hydraulic resistance.
3. Hydraulic Manifold Block & Proportional Valving
Hydraulic efficiency and cycle speeds depend on fluid circuit design. Pipe-connected valves frequently leak under continuous 250–315 bar industrial pressure cycles. NCT presses utilize monobloc forged steel manifold blocks mounted directly on the oil tank:
- Cartridge logic valves (Rexroth / Yuken standard) minimize fluid turbulence and eliminate external piping joints.
- Pre-fill valves (suction valves) allow gravity fluid entry into the main cylinder during rapid approach, switching seamlessly to high-pressure power stroke upon material contact.
- Dual electrical safety monitored valves on the ram downstroke circuit prevent gravity falling in compliance with international CE machinery safety directives.
4. Tonnage and Stroke Sizing Matrix
| Application | Recommended Frame | Tonnage Range | Key Operational Feature |
|---|---|---|---|
| Scaffolding Ledger & Prop Pressing | C-Frame | 50 – 150 Tons | High cycling speed (25–35 strokes/min), rapid approach |
| Deep Drawn Cookware / Auto Filter Bowls | 4-Pillar Double Action | 150 – 500 Tons | Hydraulic cushion, precise blank holder tonnage control |
| Heavy Plate Straightening & Bending | H-Frame Gantry / Bed | 200 – 1000 Tons | Wide bed daylight, traveling ram cylinder carriage |
| Powder Compacting / Forging Sizing | H-Frame Straight Side | 300 – 1500 Tons | Rigid 8-point gib guideways, pressure dwell timers |
5. Factory Inspection & Delivery
Review standard and custom tonnage specifications in our hydraulic press machines division. All NCT hydraulic cylinders are machined from seamless forged ST52 steel tubes, micro-honed to Ra < 0.2 µm, and fitted with Parker / Merkel polyurethane seal packs. Machines undergo a continuous 4-hour full-tonnage pressure-hold trial before crating and export dispatch.
Senior Machine Tool Design & Production Engineering Division, Ludhiana Works
Authored by machine tool builders at our Ludhiana manufacturing works. Every technical parameter, metallurgy guideline, electrical formula, and production cycle stated in this guide is reviewed by our shop-floor engineers who assemble, wire, and execute material trials before global dispatch to GCC and domestic manufacturing facilities.
Need Engineering Consultation on This Subject?
Speak directly with National Cutting Tools senior machinery engineers.