Technical setup guide for automatic scaffolding ledger end dual-torch welding SPM. Gas shielding ratios, pneumatic clamping chucks, weld penetration, and cycle time benchmarks.
Scaffolding ledgers (horizontal transoms) are the highest volume fabricated component in any modular scaffolding system. A standard construction bay requires up to four ledgers for every vertical standard. Each ledger consists of a 48.3 mm OD steel tube with drop-forged ledger end blades welded onto both extremities.
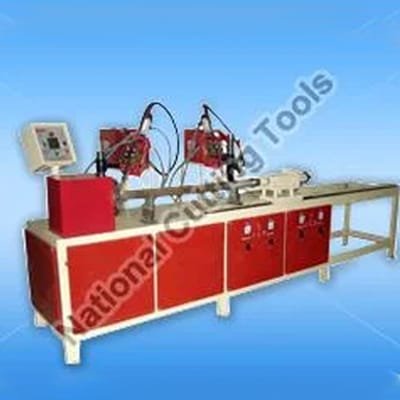
Manual welding of ledger blades creates severe production bottlenecks, irregular weld thickness, and high rejection rates during mandatory site drop-hammer and tensile pull testing. National Cutting Tools engineers specialized automatic dual-torch MIG welding lines that weld both ends simultaneously in a single automated cycle.
Dual-Torch Simultaneous Welding Mechanics
Our dedicated Scaffolding Ledger End Welding Machine eliminates manual handling during welding:
- The operator loads the cut tube (0.5m, 1.0m, 1.5m, 2.0m, or 2.5m length) onto the machine bed and inserts the two forged blades into the tube ends.
- Dual pneumatic chucks activate via foot pedal, clamping the tube concentric and pressing the forged blades tight against the internal tube shoulder under 8 bar pneumatic force.
- Two heavy-duty 400A MIG welding torches strike an arc simultaneously. The motorized central head rotates the assembly through 360 degrees plus a 15-degree overlap at precision speed controlled by an AC variable frequency drive (VFD).
- Both circular welds finish in 14 to 18 seconds. Total cycle time, including pneumatic loading and unloading, is under 30 seconds per ledger.
Welding Parameters for BS 1139 & EN 12810 Compliance
To pass certified weld throat and tensile pull audits, machine settings must be strictly maintained:
| Parameter | Recommended Setting | Quality Impact |
|---|---|---|
| Shielding Gas Mixture | 80% Argon + 20% CO2 | Minimizes spatter, guarantees deep root penetration |
| Welding Wire Specification | 1.2 mm ER70S-6 copper coated wire | High tensile yield strength exceeding parent tube |
| Arc Current & Voltage | 210 to 240 Amps @ 23 to 26 Volts | Full penetration into 3.2 mm tube wall without blow-through |
| Hourly Production Output | 90 to 120 completed ledgers/hour | Replaces 4 manual welding booths with 1 machine |
Eliminating Weld Porosity on Scaled ERW Tube
Our machine design includes an automatic pre-flow gas cycle that flushes atmospheric air and loose scale off the joint for 0.6 seconds prior to arc ignition. Combined with calibrated torch lead angles, the weld puddle stays fully shielded, eliminating pinholes and porosity defects.
Visit our Ludhiana works to inspect the ledger welding line in action or test your own tube samples. Call +91-9888210800 to discuss machine delivery and custom fixture options.
Senior Machine Tool Design & Production Engineering Division, Ludhiana Works
Authored by machine tool builders at our Ludhiana manufacturing works. Every technical parameter, metallurgy guideline, electrical formula, and production cycle stated in this guide is reviewed by our shop-floor engineers who assemble, wire, and execute material trials before global dispatch to GCC and domestic manufacturing facilities.
Need Engineering Consultation on This Subject?
Speak directly with National Cutting Tools senior machinery engineers.