 Heavy Industrial SPM
Model: NCT-SPM-41
Comprehensive Machine Overview
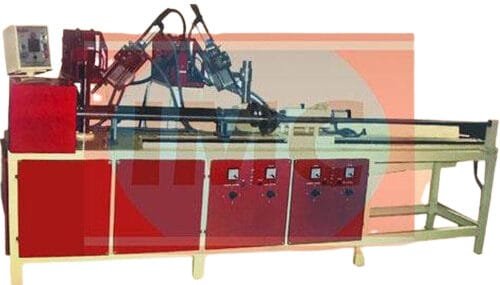
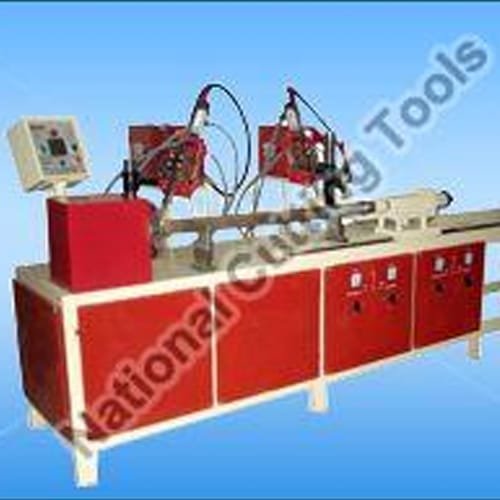
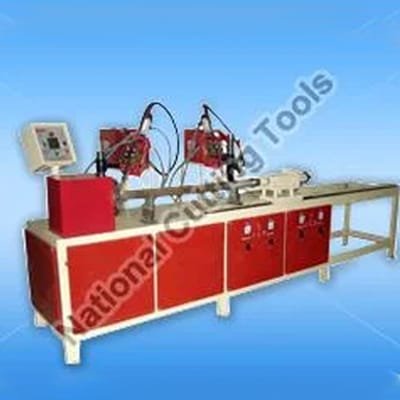
Built on a heavy structural frame to eliminate vibration harmonics and maintain precision, the Ledger Welding Machine manufactured by National Cutting Tools delivers <p>The Ledger Welding Machine by National Cutting Tools is an automated production workstation engineered for circumferential fillet welding of cast or forged steel end blades onto tubular scaffolding ledgers. In modular scaffolding systems like Cuplock, Kwikstage, and Ringlock, ledgers act as horizontal ties; weld integrity at the blade-to-pipe junction is vital to resist tensile pull-out and bending moments during service.</p>.
<p>The machine uses a heavy horizontal steel bed with a motorized rotary headstock and an adjustable tailstock carriage. Pneumatic jaws clamp the cut-to-length 48.3 mm OD tube while precision locator fixtures hold the end blades in true axial alignment. Dual welding torches initiate simultaneously, laying down clean, spatter-free circular welds around both ends in a single automated cycle taking under 40 seconds.</p>
<h3>Key Features</h3>
<ul>
<li><strong>Simultaneous Dual-End Welding:</strong> Two independent MIG torches weld both end connectors simultaneously, balancing heat input and cutting cycle time by half.</li>
<li><strong>Interchangeable Blade Tooling:</strong> Drop-in locator jaws accommodate forged Cuplock ledger blades, Ringlock cast wedge heads, and Kwikstage captive wedges.</li>
<li><strong>Adjustable Length Carriage:</strong> Smooth-sliding tailstock assembly on machined ways accommodates ledger lengths from 0.4 m up to 2.5 m with positive mechanical stops.</li>
<li><strong>Rotary Inverter Drive:</strong> Variable frequency drive allows smooth speed control from 2 to 12 RPM to match pipe wall thickness and wire diameter.</li>
<li><strong>Pneumatic Clamping Sequence:</strong> Foot-switch activated pneumatic cylinders clamp the pipe and lock end fittings in place before arc initiation.</li>
<li><strong>Spatter Protection Guards:</strong> Heavy acrylic and sheet metal sliding hood protects the operator from glare and contains welding fumes and spatter.</li>
</ul>
<h3>Applications</h3>
<ul>
<li>Fabrication of Cuplock forged-blade horizontal ledgers</li>
<li>Ringlock cast-head ledger and transom welding</li>
<li>Kwikstage horizontal ledger and tie bar production</li>
<li>Circular tube-to-fitting welding in structural steel workshops</li>
</ul>
<p>Manufactured at the NCT engineering works in Ludhiana, Punjab. Every machine is tested for spindle alignment, weld bead uniformity, and pneumatic clamping force before being packed for delivery across India or for overseas container export.</p>
High-Yield Production Capabilities & Advantages
Simultaneous Dual-End Seam Welding
Two synchronized welding torches operate at both ends of the ledger pipe simultaneously, eliminating manual flipping and cutting handling time by over 60%.
18–24s Rapid Cycle Time per Ledger
Produces 120 to 160 finished ledgers per hour at 85% operator efficiency, replacing 4 to 5 manual welding booths while using 80% less shop floor space.
4.0–5.5 mm Controlled Penetration
Continuous motorized rotation guarantees uniform fillet throat thickness with zero stop-start cold laps, passing rigorous pull-out and shear load tests.
Zero Spatter on Forged Blade Locking Pockets
Precision wire feed control and tailored shielding gas shrouds protect blade locking pockets from spatter, eliminating manual chiseling before galvanizing.
Pneumatic Rapid Clamping & Ejection Cradle
Heavy pneumatic cylinders secure both ledger heads in 1.5 seconds. A post-weld pneumatic lift cradle unloads finished ledgers directly onto gravity transfer tables.
Engineering Data Matrix
| Technical Parameter | Operational Specification / Value |
|---|---|
| Electric Supply | Single Phase 220 Volt HZ 50/60 |
| Speed | 2 To 10 rpm |
| Motor Drive | AC Inverter Type |
| Motor-Type | AC 220-Volts-3-Phase |
| Torch Clamping | PNEUMATIC |
| Length Adjustment | 150 To 2400 Mm |
| Dimension | L X W X H 11.3×2.5×5.3 (Foot) |
Machine Architecture & Mechanical Construction
Stress-Relieved Machine Bed (IS 2062)
Heavy-duty chassis fabricated from IS 2062 structural steel channels and 25 mm thick ground steel plates. Thermally stress-relieved prior to multi-axis plano-milling.
Hardened Spindle & Precision Headstock
Induction-hardened EN8/EN9 alloy steel main spindle on heavy tapered roller bearings, driven by a 1.5 HP motor and Delta VFD for backlash-free rotational starts and stops.
Tailstock & Quick-Change Ledger Tooling
Adjustable tailstock on induction-hardened guide shafts. Drop-in, case-hardened alloy tool-steel fixtures accommodate Cuplock blades, Ringlock heads, or Kwikstage wedges in under 10 minutes.
IP54 Dust-Proof Industrial Electrical Cabinet
Isolated, forced-air cooled IP54 electrical enclosure housing Delta/Mitsubishi PLC, touch HMI screen, and universal dry-contact trigger interfaces for Lincoln, Panasonic, and Kemppi.
Industrial Plant Integration & Fabrication Flow
Balanced production beat eliminating fabrication queue bottlenecks.
Precision Pipe Cutting
Cold saw cutting of raw IS 2062 / EN 10219 pipe into exact ledger lengths (500 mm – 3000 mm) with 90° square cut faces.
Pipe End Chamfering
Automatic pipe end-facing removes inner and outer burrs, ensuring 100% flush root fit-up against forged blade weld shoulders.
Dual-Torch MIG Welder
NCT dual-torch SPM strikes simultaneous arcs, completing twin 360°+15° circumferential welds within 18–24 seconds.
QA & Galvanizing
Batch tensile pull testing followed by immediate transfer to acid pickling and molten zinc hot-dip galvanizing baths.
Ledger Welding Machine Works QA & Export Packaging Protocol
✓ Circumferential Arc & Pneumatic Alignment Trials
- • Rotary Spindle Concentricity: Spindle chuck and pneumatic tailstock axial alignment verified within 0.08 mm to ensure uniform rotation without tube run-out.
- • Continuous Arc Cycle Testing: Minimum 25 continuous 360-degree weld runs executed on sample pipes to verify torch angle, arc stability, and bead penetration.
- • Macro-Etch Penetration Check: Cut-section metallurgical inspection of weld beads to confirm root penetration meeting BS 1139 and EN 12810 standards.
- • Run-Off Video Recording: Trial welding cycle on your specified tube diameter recorded in HD and shared for formal technical sign-off prior to dispatch.
Seaworthy Automated Station Packaging (ISPM-15)
- • Torch Carriage Bracing: Pneumatic slides, welding torch brackets, and rotary spindles locked with heavy-duty mechanical transport braces.
- • VCI Moisture Protection: Copper heat sinks, clamping jaws, and bare electrical contacts treated with volatile corrosion inhibitor (VCI) film.
- • Solid Timber Crating: Fumigated ISPM-15 certified solid pine wood crate with waterproof polyethylene outer envelope.
- • Container Lashing Points: Heavy structural skid base with internal corner tie-down brackets for ocean container transport.
International Shipping Destinations & India Supply Network
National Cutting Tools manufactures and configures the Ledger Welding Machine for seamless integration into international fabrication lines and domestic scaffolding manufacturing plants. All machinery is customized for local electrical grids, certified for regional compliance, and dispatched with seaworthy protective packaging.
Primary International Export Destinations
All Export Hubs →Pan-India Fast Freight Dispatch (Ludhiana Works)
India Directory →Full-truckload (FTL) and part-load freight dispatch directly from our central manufacturing works at Focal Point, Ludhiana. Factory engineers provide on-site leveling, tool alignment, and operator training across all major industrial manufacturing clusters:
Frequently Asked Questions • Ledger Welding Machine
Direct Factory Machinery Proposal
Connect with our engineering specialists in Ludhiana. Receive comprehensive technical specifications, power requirements, tooling options, and estimated FOB/CIF maritime rates.
Request Formal Quotation
Please provide production requirements for exact tooling design.
Scaffolding Manufacturing Machinery: The Complete Plant Setup Guide
Technical breakdown covering machine sizing, tooling die setups, cycle speeds, and operational maintenance for Scaffolding Machinery.