Manufacturing workflow for telescopic scaffolding props (Acro props). Explains inner pipe multi-hole punching, outer sleeve cold thread rolling, and base plate welding.
Telescopic Steel Prop Manufacturing Workflow
Adjustable scaffolding props (commonly known as Acro props) consist of an outer tube (typically 60.3mm O.D.) and an inner telescoping tube (48.3mm O.D.). Manufacturing props at volume requires dedicated cold forming equipment to achieve high load ratings under EN 1065 Class C/D/E requirements.
Threaded Sleeve Cold Rolling vs Cut Threads
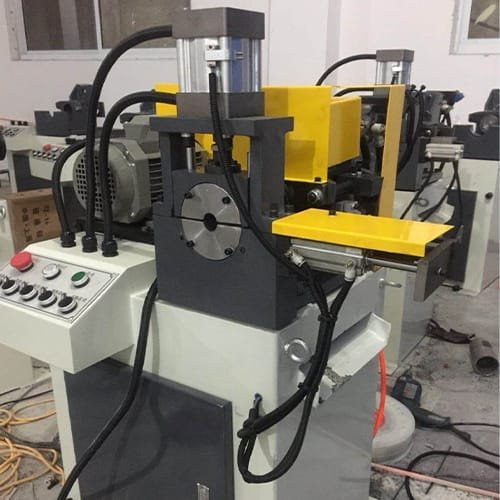
The adjustment sleeve must never feature machine-cut threads because cutting removes parent steel and weakens the thin tube wall. Our Scaffolding Prop Thread Rolling Machine utilizes cold roll-forming dies that displace grain structure, increasing surface hardness by 15-20% and preserving full tensile strength.
| Component Stage | Tooling Machine | Key Metric |
|---|---|---|
| Outer Tube Thread Sleeve | Prop Thread Roller | 8 TPI or 4 TPI Heavy ACME / Trapezoidal |
| Inner Tube Adjustment Holes | Hydraulic Hole Puncher | 14mm / 16mm Holes at 100mm Pitch |
| Sleeve Slotted Handle Hole | Rotary Slot Punch | Accurate collar handle clearance |
| Base & Top Plates | Pillar Power Press | 150x150x6mm Embossed Square Plates |
For high-speed shearing of outer and inner tubing prior to thread forming, fabricators utilize our Semi Automatic Pipe Cutting Machine for clean, chip-free cuts.
Machines covered in this guide
Senior Machine Tool Design & Production Engineering Division, Ludhiana Works
Authored by machine tool builders at our Ludhiana manufacturing works. Every technical parameter, metallurgy guideline, electrical formula, and production cycle stated in this guide is reviewed by our shop-floor engineers who assemble, wire, and execute material trials before global dispatch to GCC and domestic manufacturing facilities.
Need Engineering Consultation on This Subject?
Speak directly with National Cutting Tools senior machinery engineers.